- 24/7
Customer Service
- IBR Certified
Manufacturer
- Qualified
Expert Professional
Fully Wetback Boilers Manufacturer in India
Highly Efficient Fully Wetback Steam Boilers for Industrial Purposes
Himani Boiler is known as one of the best Fully Wetback Boiler Manufacturers in India, providing efficient, energy-saving and durable industrial steam boilers. Made especially for industrial processes, our fully wetback boilers concentrate on the issues of efficient heat transfer, constant steam generation and overall performance of the system.
Having more than 35 years of experience in the industrial boilers manufacturing industry, Himani Boiler provides custom-made boilers according to the industrial heating needs of the customers. Our highly experienced engineers, good manufacturing practices and reliable after-sales services provide all the necessary assistance when you are looking for a reliable industrial boiler solution.
If you need a boiler for food industry, textile industry, chemical industry, plywood industry or any other purpose, we will be able to help you choose an appropriate boiler depending on your steam capacity and operating pressure.
Get a QuoteWhat Is a Fully Wetback Boiler?
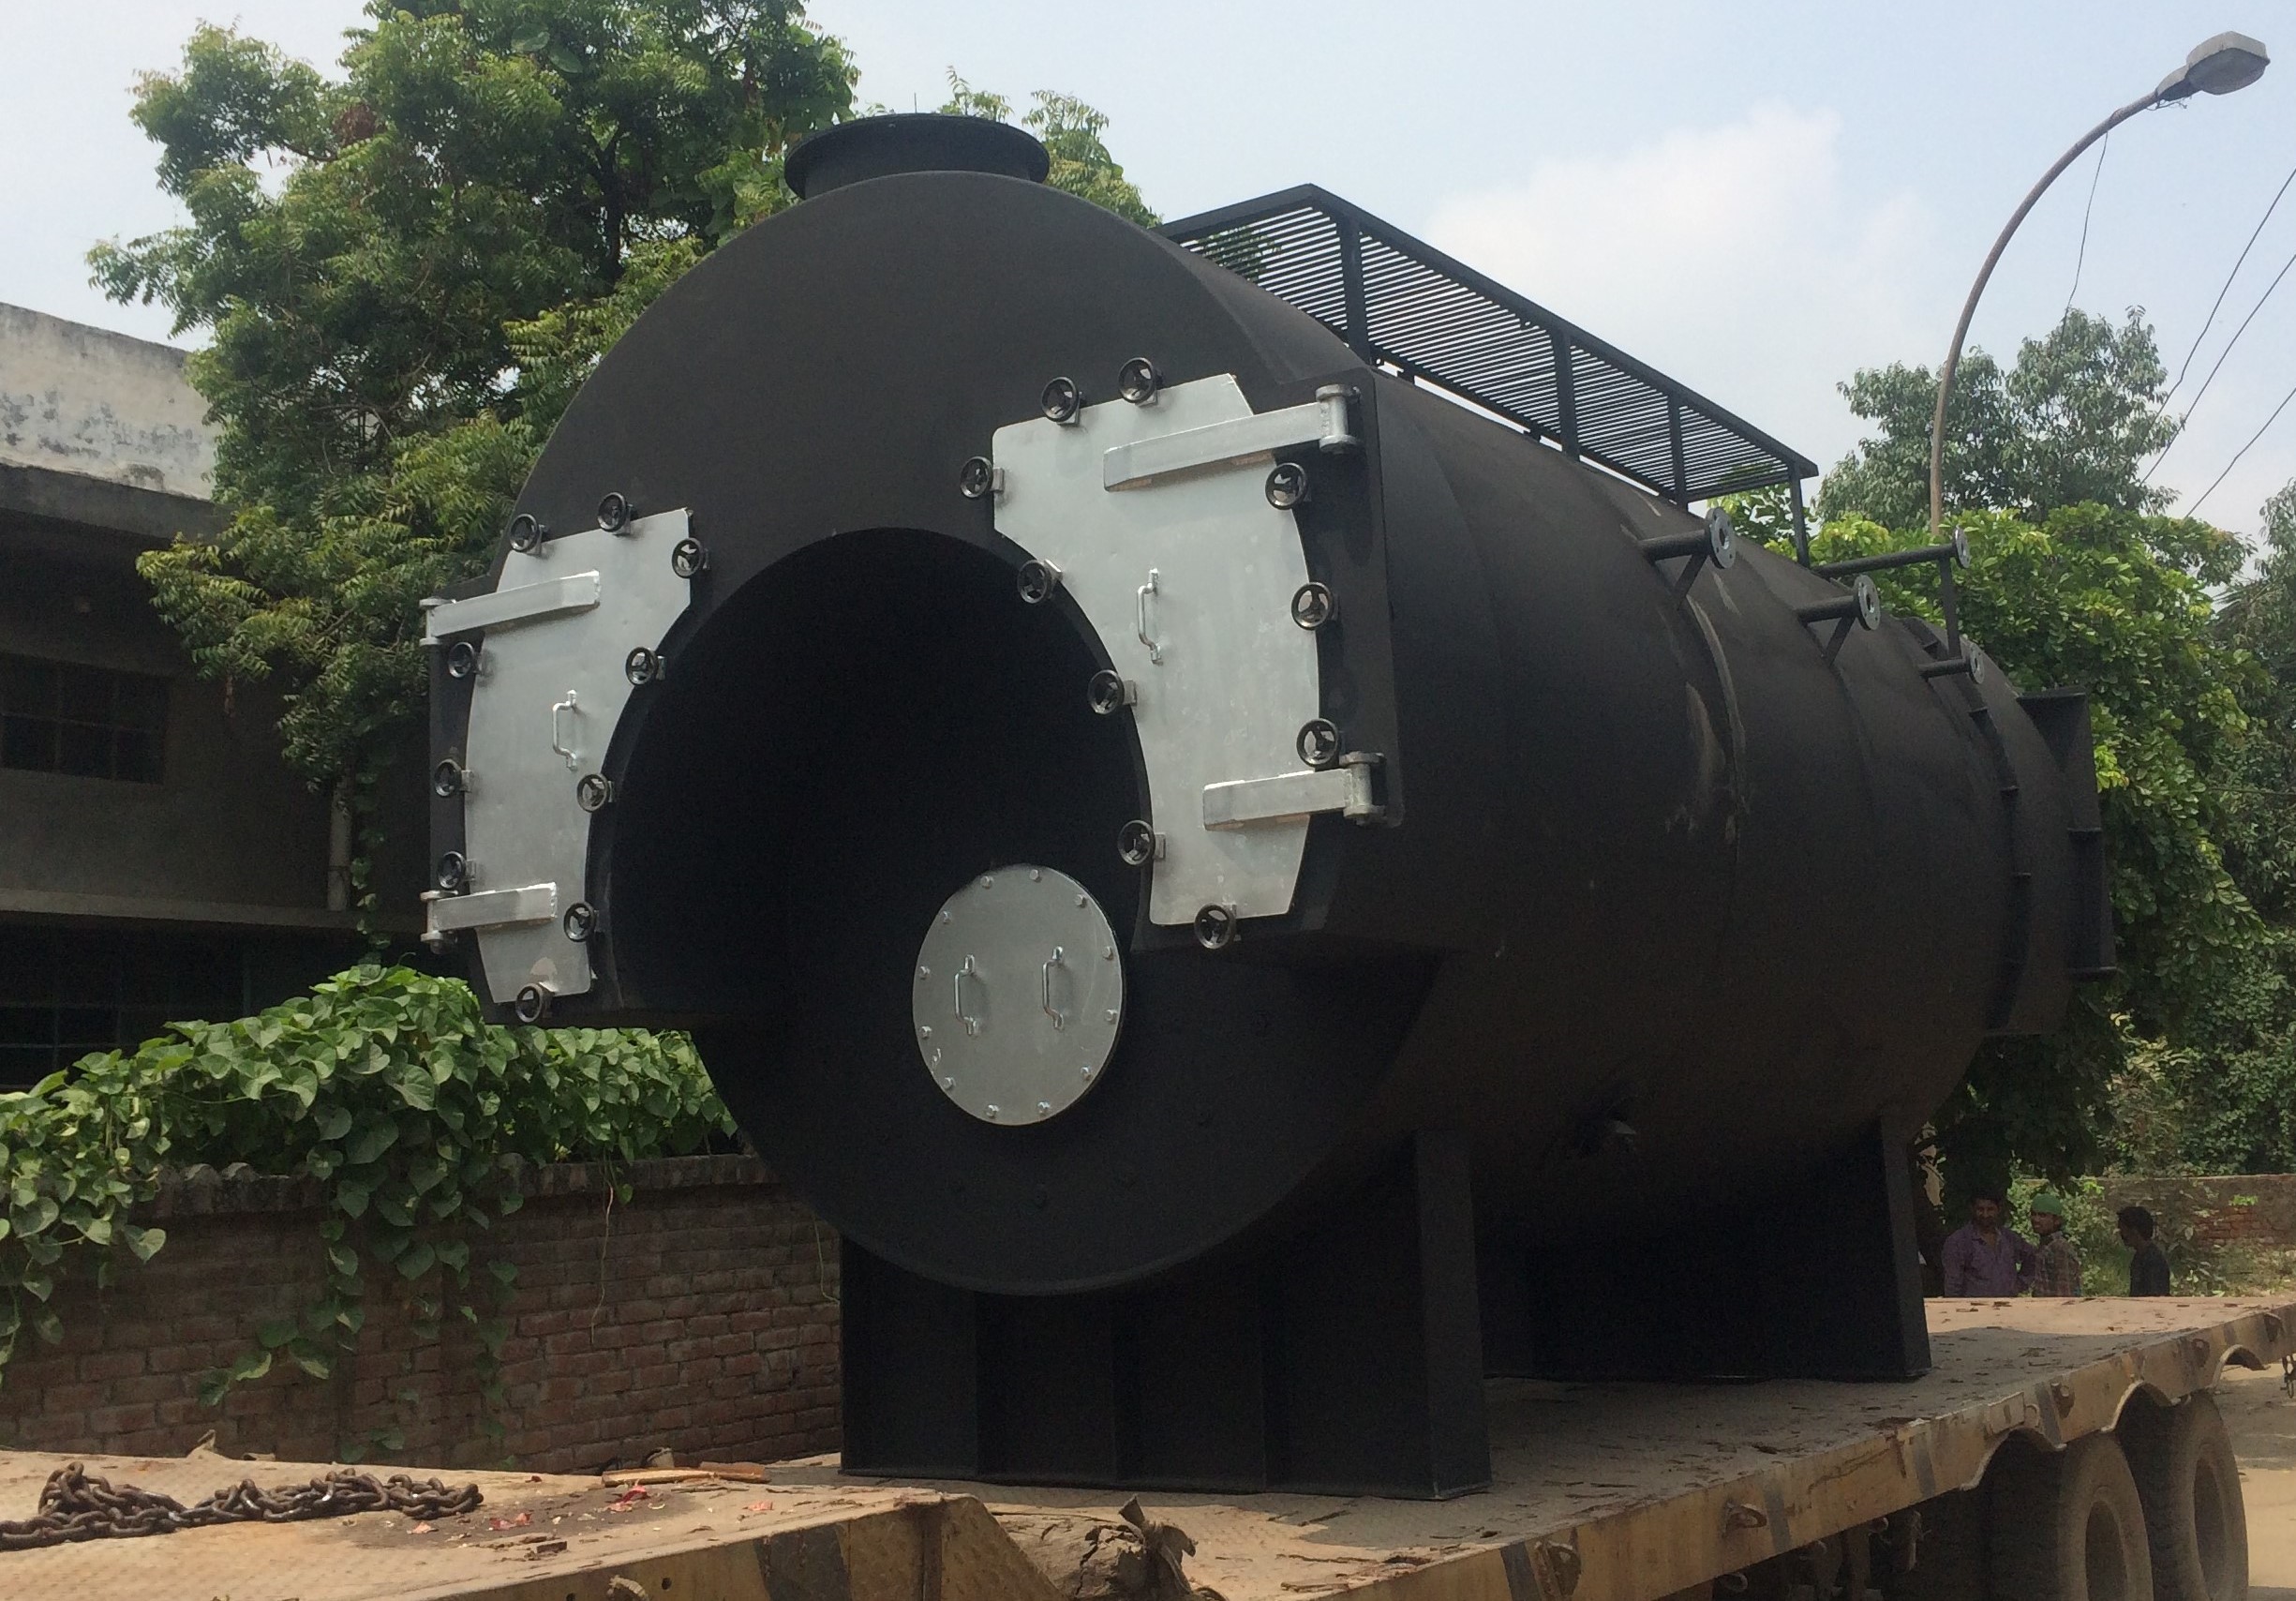
Wetback Boilers Wetback Boiler refers to a Fire Tube Boiler design in which the turnaround space at the back is fully enveloped in boiler water. In such a boiler, the reversal of flue gases takes place in a water-cooled space after which it moves into the other flue spaces.
By having a wetback boiler, heat losses from the back end can be minimized. Based on the particular boiler design, one can get a boiler with high efficiency, good steam production, and low maintenance needs.
Wetback boilers are applied in many industrial sites where there is a need for continuous steam production.
Key Features of Himani Fully Wetback Boilers
Fully Water-Cooled Rear Chamber
The wetback design incorporates a water-cooled rear turnaround chamber, helping minimize heat loss from the rear section and supporting efficient thermal operation.
Efficient Heat Transfer
The boiler's multi-pass flue gas arrangement enables effective heat exchange between hot combustion gases and boiler water, supporting fuel-efficient steam generation.
Robust Industrial Construction
Manufactured using quality materials and established fabrication practices, our boiler solutions are designed to withstand demanding industrial operating conditions.
Consistent Steam Generation
Engineered according to the required steam load and operating parameters, fully wetback boilers can support continuous industrial processes requiring a dependable steam supply.
Flexible Fuel Options
Depending on the selected boiler configuration, fuel options can include oil, gas or suitable solid fuels. Fuel compatibility is finalized according to the combustion system and project requirements.
Convenient Inspection and Maintenance
The boiler arrangement can be designed to facilitate access to key components for inspection, cleaning and routine maintenance, helping support long-term operational reliability.
Customized Engineering
Himani Boiler provides customized industrial boiler solutions based on steam capacity, operating pressure, fuel availability, plant layout and process requirements.
Advantages of Fully Wetback Boilers
Choosing a fully wetback boiler can offer several operational advantages for industrial facilities.
Improved thermal performance: The water-cooled rear chamber and multi-pass heat transfer arrangement help optimize the use of combustion heat.
Reduced heat loss: The wetback configuration minimizes direct heat exposure at the rear turnaround chamber.
Fuel efficiency: An appropriately engineered boiler, combined with suitable combustion controls and regular maintenance, can help optimize fuel consumption.
Reliable operation: Robust construction and suitable safety systems support dependable performance under specified operating conditions.
Reduced maintenance requirements: The absence of a refractory-lined rear turnaround chamber in the wetback design can reduce refractory maintenance associated with conventional dryback configurations.
Industrial versatility: Suitable configurations can be engineered for a wide range of manufacturing and process heating applications.
Long-term value: Efficient operation, appropriate maintenance and durable construction can contribute to lower lifecycle operating costs.
Actual efficiency, fuel savings and maintenance requirements depend on boiler capacity, fuel quality, operating conditions and system configuration.
Technical Specifications of Fully Wetback Boilers
Himani Boiler offers customized industrial boiler engineering based on individual project requirements. The following are the key parameters considered when selecting a fully wetback boiler.
| Parameter | Description |
|---|---|
| Boiler Type | Fully Wetback Fire-Tube Steam Boiler |
| Design | Water-cooled rear turnaround chamber |
| Configuration | Multi-pass, as per design |
| Fuel Type | Oil, gas or suitable solid fuel, subject to configuration |
| Steam Capacity | Customized as per industrial requirements |
| Operating Pressure | As per process requirements and applicable regulations |
| Construction | Industrial-grade materials and engineered fabrication |
| Applications | Manufacturing, processing and industrial heating |
| Safety Systems | As per applicable boiler regulations and project specifications |
| Installation | Based on site and project requirements |
Why Choose Himani Boiler for Fully Wetback Boilers?
Over 35 Years of Industrial Experience
Established in 1991, Himani Boiler brings decades of experience in manufacturing industrial boilers and thermal solutions for diverse industries.
Customized Boiler Engineering
Our engineering team considers your plant's steam demand, fuel availability, operating pressure and installation requirements to develop a suitable boiler solution.
Quality-Focused Manufacturing
We emphasize quality raw materials, reliable fabrication practices and manufacturing checks to deliver durable industrial boiler systems.
Energy-Efficient Solutions
Our boiler designs focus on effective heat transfer and optimized combustion to support improved fuel utilization and operational efficiency.
Installation and Commissioning Support
We provide project-based technical assistance to help customers with boiler installation, commissioning and operational requirements.
Dependable After-Sales Service
Our support includes technical guidance, maintenance assistance and spare parts support to help maintain long-term boiler performance.
Our Fully Wetback Boiler Manufacturing Process
At Himani Boiler, we follow a systematic approach to deliver industrial boiler solutions suited to individual plant requirements.
Requirement Analysis
Understanding the customer's steam demand, fuel type, operating pressure and industrial application.
Engineering and Design
Developing the boiler configuration according to the specified technical and operational requirements.
Fabrication and Manufacturing
Manufacturing the boiler using suitable materials and established fabrication procedures.
Quality Inspection
Conducting applicable manufacturing inspections and testing as per the approved design and regulatory requirements.
Installation and Commissioning
Providing project-specific support for installation and commissioning.
After-Sales Assistance
Offering technical guidance, maintenance support and assistance with spare parts.